Mechanical
Map actual conveyor dimensions, product presentation, spacing and tag position, including surrounding tagged stock. Include operator, cleaning and maintenance access in the read-point layout.
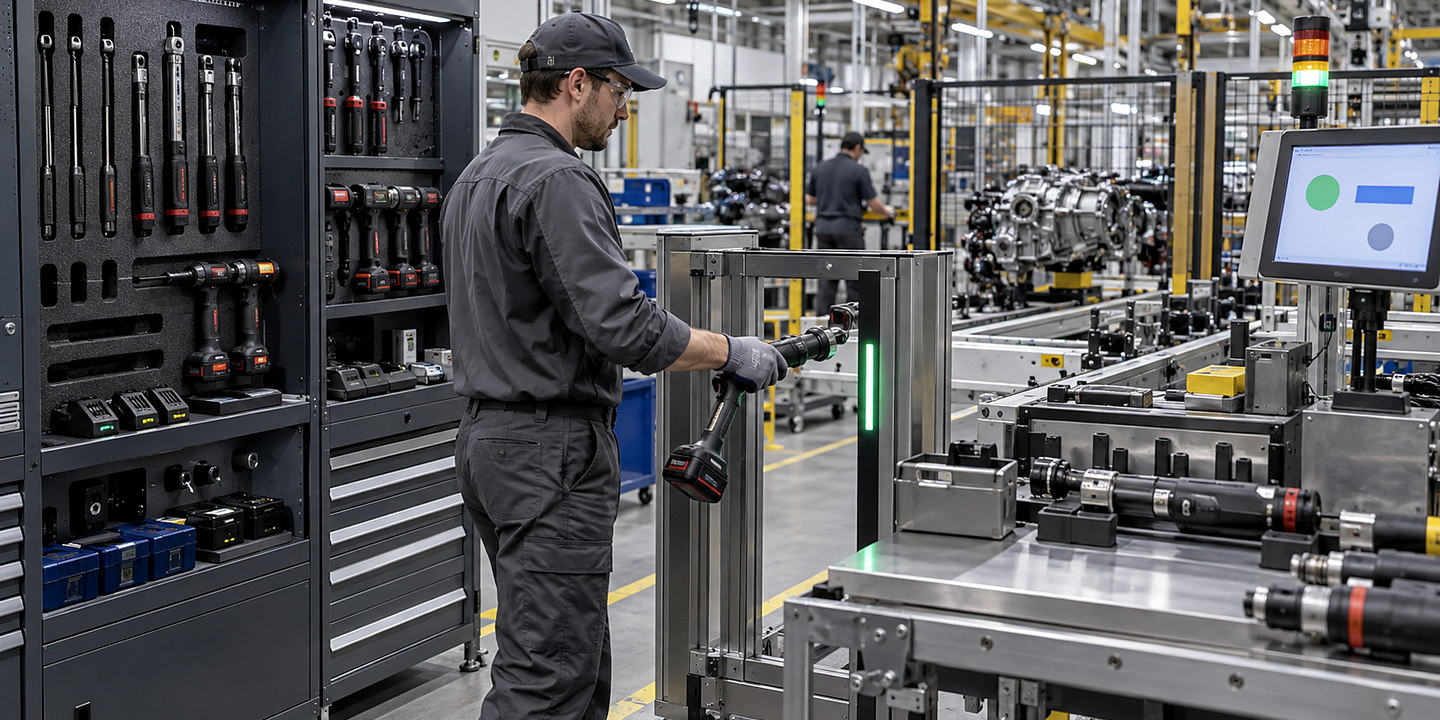
Define conveyor RFID interfaces for passing groups, conveyor states, accepted tracking events, acknowledgements, exceptions and controlled recovery.
Connect the agreed passing-group definition to actual conveyor states and the event received by the tracking system. Define when a result is accepted, how it is acknowledged and what happens to an unresolved group during a stop, repeated pass, communication fault or restart.
Document the tag, group and event definitions in the interface brief. Do not assume a detected tag set proves the physical group, correct business data or a completed handover.
Plan controlled conveyor RFID read zones around your identifiers, substrates, production events, system interfaces, exceptions and verification records. Discuss a practical data-flow approach with Oxford Traceability. Your integration review should connect production speed and read-point conditions, line, business-system and network interfaces and the people who run the process.
Discuss your application

Map actual conveyor dimensions, product presentation, spacing and tag position, including surrounding tagged stock. Include operator, cleaning and maintenance access in the read-point layout.
For Controlled Conveyor RFID Read Zones, list the supplies, isolation, protective devices, panels and cable routes required by the proposed installation.
Agree the conveyor states and confirmation that define a passing group. Specify the response to incomplete or unwanted results, repeated movement, stops and controlled restart; do not assume a particular interlock or reject mechanism.
Review risk controls, stop behaviour, access, reset and the checks needed around line, business-system and network interfaces.
Define expected identities, observed tag sets, group and event identifiers, acceptance and acknowledgement. Assign ownership of late or repeated events, unresolved results and authorised corrections.
Name who resolves missing or unwanted reads and reconciles the physical group with the tracking record. Train for reworked/repeated passes, access, faults and controlled recovery using agreed trial cases.
For Controlled Conveyor RFID Read Zones, your team can review each stage before the complete installation is put into routine use.
Share real identifiers, substrates, production events and exception records, including the normal range for identifier and data rules for controlled conveyor RFID read zones and the difficult substrate, label or tag behaviour cases.
Compare suitable methods and use focused trials to show how each option performs against production speed and read-point conditions.
Connect the equipment to your line, services and controls while resolving line, business-system and network interfaces for day-to-day operation.
Confirm exception, rework and duplicate handling, then complete and record verification, retention and reconciliation evidence before your operating team takes over.
For your application: check production speed and read-point conditions, line, business-system and network interfaces, exception, rework and duplicate handling, and verification, retention and reconciliation evidence as part of the complete line trial.